
 中文简体
 русский
 Français
 Español
 Português
 Deutsch
 عربى
 italiano
 Türk
Search
Categories
Recommend News
Categories
Recommend News
-
Industry News
-
Industry News
-
Industry News
-
Industry News
Oct 19, 2026 - By admin
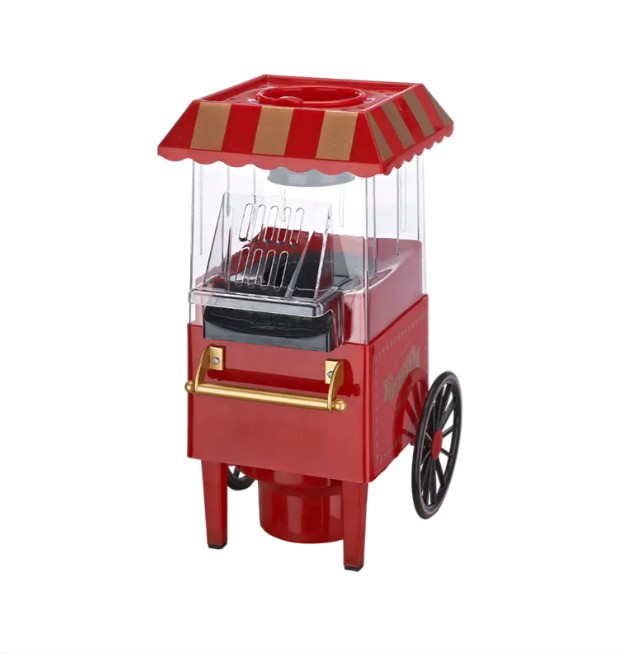
How to Use a Compact Hot Air Popcorn Maker: Setup, Tips, and Care Guide
On a countertop no wider than a cutting board, a compact hot air popcorn maker can turn a third of a cup of kernels into a bowl of popcorn in about two and a half minutes. The first kernel usually cracks within 45 to 60 seconds after the fan and heating element come on. If you have ever stood in front of one of these machines wondering why the batch came out chewy, why kernels shot across the counter, or why the popping stopped before the bowl was full, the answer is rarely complicated. The machine is simple; the variables are dose, airflow, and moisture.
This guide explains how to use a compact hot air popcorn maker from first plug-in to final cleanup. It covers the starting batch size, the stopping point, the reasons kernels escape the chamber, the kernel specs that matter, and the buying questions that retailers and food-service operators should ask before placing an order. The advice is written for home users who want a repeatable bowl, and for commercial buyers who need a predictable machine for a retail shelf, a rental counter, or a small food-service operation.
The short version is this: measure the kernels, keep the chamber upright, listen for the slowing pop, and clean the machine while it is still easy to wipe. A compact hot air popper does not need oil in the popping chamber, does not need a preheat cycle longer than a minute, and does not benefit from a full hopper. It rewards consistency more than technique.
A compact hot air popper works best when you treat batch size, airflow, and kernel moisture as fixed inputs, not as things to adjust after the first batch goes wrong.
How to Use a Compact Hot Air Popcorn Maker Step by Step
Start with the machine on a level, dry surface. Leave at least two to three inches of clearance around the air vents and keep the unit away from the edge of the counter. A hot air popper pulls air through the base and pushes it up through the popping chamber; a towel, a sink mat, or a crowded shelf can block that flow and make the batch uneven. Plug the unit in with dry hands and keep the cord away from the hot air outlet.
Measure the kernels before you turn the machine on. Most compact hot air poppers are designed around a third of a cup of kernels, which weighs roughly 60 to 80 grams depending on the kernel size. Use the measuring cup that came with the machine if one is supplied, or use a dry measuring cup and level it off with a knife. Do not heap the cup and do not pour kernels straight from the bag. A heaped cup can add 20 to 30 percent more kernels than the chamber can move, and that extra volume is the most common cause of unpopped kernels, slow popping, and kernels flying out of the chute.
There is no need to preheat an empty chamber for several minutes. The heating element and fan work together from the moment you switch the unit on. Adding kernels at the start gives them the most even exposure to the rising air. If your manual recommends a short warm-up, keep it to 30 to 60 seconds and never leave the machine running empty for long enough to smell hot plastic or scorched metal.
Turn the machine on, add the measured kernels through the chute, and fit the lid or butter tray according to the manual. The first pop usually arrives within 45 to 60 seconds. Let the machine run until the popping slows to about one pop every two to three seconds. That is the practical stopping point. Waiting for every last kernel to pop often produces a burnt taste, because the kernels that remain are usually too dry or too small to pop, and the chamber keeps heating them while the edible popcorn sits against the hot air stream.
Switch the unit off before you remove the lid. Steam collects under the lid and around the chute, so lift the lid away from your face and let the popcorn fall into a bowl. If the machine has a butter tray, remove it with a cloth or oven mitt because it will be hot. Let the unit cool completely before you wipe the chamber or store it. A compact hot air popper is not a heavy-duty commercial machine; giving it a few minutes to cool between batches is cheaper than replacing a thermal fuse.
The most reliable stopping point is sound, not the clock: cut the power when you hear two to three seconds between pops.
Batch Size, Bowl Capacity, and the Risks of Overfilling
Batch size is the first number to lock down. A third of a cup is a common starting point for compact hot air poppers because it gives the fan enough space to move every kernel and gives the heating element enough airflow to carry heat evenly. That batch usually yields six to seven cups of popped corn. A quarter cup yields four to five cups and is a safer choice for very small machines or for kernels that are on the large side. A half cup can work in a larger tabletop model, but in a compact chamber it often leads to a dense kernel mass that the air cannot lift.
Overfilling does not just reduce yield. It changes the way the machine behaves. Kernels that cannot circulate sit against the hot chamber wall and scorch on one side while remaining unpopped on the other. The fan has to push against a heavier load, so the airflow slows, the chamber temperature rises, and the machine may trip a thermal cutout. In a retail or food-service setting, that kind of abuse shortens the duty cycle and increases return rates. For a home user, it usually means a bowl of half-popped kernels and a machine that smells burnt for the next three batches.
| Kernel volume | Approximate weight | Popped yield | Risk level |
|---|---|---|---|
| 1/4 cup | 45 to 60 g | 4 to 5 cups | Low; good for small chambers and large kernels |
| 1/3 cup | 60 to 80 g | 6 to 7 cups | Standard; best balance of airflow and output |
| 1/2 cup | 90 to 120 g | 9 to 10 cups | High in compact models; uneven pop and overheating risk |
Use the table as a starting point, not as a guarantee. A machine rated at 1,200 watts with a wide chamber may handle a half cup better than a 700-watt compact unit with a narrow chute. The manual is still the first authority. If the manual says one-third cup, do not treat a half cup as an upgrade. Treat it as a different machine class.
Stay at or below the manufacturer's marked line; a full chamber is not a faster batch, it is an uneven one.
Why Kernels Fly Out and How to Keep the Popping Chamber Contained
Kernels escaping the chute is one of the most common complaints about compact hot air poppers, and it is usually a symptom of airflow, not a defective machine. When the chamber is overfilled, the fan has to push harder to move the kernel mass. The resulting bursts of air can launch lighter kernels out of the chute before they have fully popped. A missing lid, a loose butter tray, or a lid that does not sit flat has the same effect. So does a batch that is too small: a few kernels in a wide chamber can bounce around and ride the air stream straight out of the opening.
Check the obvious causes first. Make sure the lid or butter tray is seated exactly as the manual describes. Confirm that the machine is on a level surface and that the vents are not blocked. Reduce the batch from one-third cup to one-quarter cup and see whether the ejection stops. If the machine has a deep chute and a shallow lid, a slight backward tilt of five to ten degrees can sometimes reduce the launch angle, but only do this if the manual allows it and only if the tilt does not expose the heating element or block the vents. Never place a cloth, plate, or foil over the chute to stop kernels; that traps heat and creates a burn risk.
Old kernels are another factor. Kernels that have dried out too much are lighter and can be tossed around more easily before they pop. If the same batch size worked last month and now kernels are flying out, test a fresh bag of kernels before you blame the machine. In a commercial setting, rotate stock and keep kernels in an airtight container away from heat. A supplier that ships kernels in a sealed, moisture-barrier bag is easier to manage than a supplier that ships in paper sacks.
If kernels escape, reduce the batch before you change the machine angle; airflow is easier to correct than a damaged fan.
Kernel Selection: Moisture, Size, and Freshness
Popcorn kernels need moisture to build pressure inside the hull. The practical target for hot air popping is about 13 to 14 percent moisture. Kernels that are too dry pop small and chewy, or they do not pop at all. Kernels that are too wet steam and clump, and they can leave a gummy residue in the chamber. You do not need a moisture meter for home use, but you do need to treat kernels as a perishable ingredient. Buy from a supplier with steady turnover, store them in an airtight container in a cool cupboard, and use them within about six months of opening.
Kernel size matters in a compact chamber. Small and medium butterfly kernels are the most forgiving because they pop quickly and fill the bowl with a light, crisp texture. Large mushroom kernels are better for coating and caramel because they hold their shape, but they need more heat and more room. In a narrow hot air chute, a large mushroom kernel may not circulate well, and the result is a batch with more unpopped kernels than a butterfly batch. If you are testing a new kernel, run a quarter-cup batch first and count the unpopped kernels. A good batch should leave no more than 5 to 10 percent unpopped. If more than 15 percent remain, check freshness, batch size, and machine clearance before you change the machine.
Color is mostly a flavor and presentation choice. Yellow kernels are the familiar all-purpose option. White kernels pop slightly larger and look brighter in a clear bag. Blue and red kernels bring a nuttier flavor and a more distinctive look, but they can be more variable in pop rate. For retail packaging, a consistent butterfly kernel with a clean yellow or white color is easier to support with a stable supply chain. For food-service, the same consistency matters more than novelty because the operator needs a predictable yield per batch.
Fresh, mid-size butterfly kernels at 13 to 14 percent moisture give the most consistent pop in a compact hot air chamber.
Butter, Oil, and Seasoning: What Belongs in a Hot Air Popper
A hot air popper is not a kettle popper. The popping chamber is designed for dry kernels and moving air. Do not pour oil into the chamber unless the manual specifically says the model has an oil-ready design. Oil in a hot air chamber can smoke, coat the fan, and leave a residue that is difficult to remove. Do not add sugar to the chamber to make kettle corn. Sugar melts, burns, and can seize the fan or the heating element. If you want caramel corn or kettle corn, use a stovetop kettle, a dedicated kettle popper, or a coated pan. The hot air machine is for plain popcorn that you season after popping.
Butter is best handled in the butter tray if your model has one. The tray sits on top of the chamber and uses the rising heat to melt butter slowly. Add butter in small pieces rather than a solid block, and do not overfill the tray. When the popping slows, remove the tray and pour the melted butter over the bowl. If you want a lighter coating, use a fine mist of oil or a small amount of clarified butter. Clarified butter has less water, so it coats the popcorn without making it soggy.
Season after popping, not during. Fine salt, nutritional yeast, paprika, and dried herbs stick better when the popcorn is still warm and slightly moist from steam. If you are seasoning for a retail or food-service application, test the coating on a small batch first. A coating that is too heavy can make the popcorn chewy within an hour, especially if it is stored in a sealed bag. A light, dry seasoning is more stable for packaging and for holding under a heat lamp.
Keep the popping chamber dry; add butter and salt after the kernels have left the machine.
Cleaning, Storage, and Daily Maintenance
Unplug the machine and let it cool before you clean it. Remove the lid, butter tray, and any removable chute parts. Wipe the outside of the base with a damp cloth and mild dish soap, then dry it immediately. Do not immerse the base in water and do not put it in a dishwasher. The heating element and fan are not sealed for immersion, and water trapped inside the housing can cause a short circuit or a musty smell on the next batch.
For the popping chamber, use a soft brush or a dry cloth to remove stray kernels and kernel dust. A vacuum with a brush attachment can help, but keep the nozzle away from the heating element. If the chamber has a nonstick coating, avoid abrasive pads and sharp tools. For the butter tray, wash it in warm soapy water and dry it fully before you put it back. A butter tray with a film of old butter can smoke on the next batch and leave a burnt taste that is hard to trace.
Store the machine with the lid off or slightly ajar so that any residual moisture can escape. Keep the cord loosely coiled rather than wrapped tightly around the base. Check the cord and plug for cracks before each use. In a commercial setting, set up a simple cleaning log: wipe the chamber after every shift, wash the butter tray after every use, and check the vents weekly. A clean machine runs cooler and pops more evenly, and it gives you a better chance of spotting a worn part before it fails during a busy service period.
A dry chamber and a clean butter tray prevent most burnt smells and sticking issues.
Troubleshooting Common Problems
Most hot air popper problems are input problems. If the machine does not pop after two to three minutes, check the power first, then the batch size, then the kernels. A thermal cutout may have tripped if the machine was run empty or overfilled. Unplug it, let it cool for 15 to 20 minutes, and try again with a quarter-cup batch of fresh kernels. If the machine hums but the fan does not move air, stop using it and have it serviced. Do not keep cycling the power to force a batch.
Slow popping usually points to old kernels, a batch that is too large, or a blocked air intake. Chewy popcorn is often caused by trapped steam: the bowl was covered too tightly, the batch was too large, or the popcorn was stored before it had cooled. A burnt smell can come from kernel dust on the heating element, butter spilled into the chamber, or a previous batch that left a film on the hot surfaces. A machine that ejects kernels is usually overfilled or missing a lid. A machine that stops mid-batch may have hit a thermal limit, or it may have a loose cord connection.
Use a process of elimination. Change one variable at a time: batch size, kernel bag, lid fit, or resting time. Keep a small notebook or a phone note for commercial use so that you can compare batches. If a machine fails the same test three times with fresh kernels and a correct batch size, it is a service issue, not a user issue. For a retailer, that distinction matters because a high return rate is often caused by unclear instructions rather than a defective unit.
Most performance complaints trace back to three inputs: batch size, kernel moisture, and airflow clearance.
Buying Guide for Retailers, Food-Service Operators, and Private Label Programs
If you are sourcing compact hot air popcorn makers for a retail program or a food-service counter, the user guide is part of the product. A clear batch line, a simple lid, and a butter tray that is easy to remove will reduce support calls and returns. Ask for the duty cycle, the wattage, the chamber volume, and the recommended batch size in grams, not just cups. Ask whether the unit is designed for intermittent home use or for a light commercial duty cycle. A machine that is rated for three batches a day is not the same as a machine that is rated for thirty.
Voltage and plug type are the next filters. A supplier that can provide 110 to 120 volt and 220 to 240 volt versions with the correct plug and certification for your market is easier to work with than a supplier that offers only one configuration. Confirm the certification documents for the destination market, the language of the manual, and the spare-parts list. A retail program needs access to replacement lids, butter trays, and measuring cups. A food-service operator needs a machine that can be wiped down quickly and a supply of parts that does not require a full-unit replacement.
At Homease, our factory in Cixi covers 20,000 square meters and runs with 300 employees. We produce popcorn makers, cotton candy makers, air fryers, chocolate fountains, ice makers, slush machines, and milkshake makers for home kitchens, party and entertainment venues, retail channels, and food-service applications. Our popcorn maker range includes hot air, retro, and tabletop models. We support custom design, new product introduction, and a production management system built around standardized operating procedures. With a daily capacity of up to 10,000 units, we can handle trial orders and repeat programs without treating either as an exception. If you need a manufacturer, supplier, or wholesaler for a private-label popcorn maker line, the conversation should start with the batch size, the target market, and the duty cycle you expect.
Need a sample or a private-label quote? Share your target market, voltage, batch size, and packaging direction with our team. We can review the right popcorn maker platform for your retail or food-service program and confirm the sample schedule before you commit to a tooling plan.
Price comparisons are useful only after the specification is fixed. A lower unit price can disappear when you add the cost of a second manual revision, a replacement lid program, or a certification gap. Ask for a pre-production sample with the final packaging and the final manual. Run a batch test at the stated batch size and time the popping cycle. Check the noise level, the lid fit, and the ease of cleaning. Those are the details that decide whether a compact hot air popcorn maker feels reliable in a customer's kitchen or on a retail counter.
For a retail or food-service program, confirm duty cycle, voltage, and spare-parts availability before you compare price.
Frequently Asked Questions
How many kernels should I put in a compact hot air popcorn maker?
Start with one-third of a cup, or 60 to 80 grams. If the machine is very small or the kernels are large, use one-quarter cup. Do not fill the chamber to the top. The fan needs space to move the kernels, and a full chamber is the most common reason for unpopped kernels and kernels flying out of the chute.
Why did my popcorn maker stop popping after one batch?
The machine may have hit a thermal cutout. Unplug it and let it cool for 15 to 20 minutes. If it starts again but stops on the next batch, check the batch size and the air vents. If it still stops with a quarter-cup batch and clear vents, have it serviced. Do not keep restarting a machine that is overheating.
Can I add butter or oil directly to the popping chamber?
No, unless the manual specifically says the model is designed for oil. A hot air popper uses dry kernels and moving air. Oil can smoke and coat the fan, and sugar can burn and seize the mechanism. Use the butter tray if your model has one, and season the popcorn after it leaves the chamber.
How long should a batch take in a compact hot air popcorn maker?
The first pop usually arrives in 45 to 60 seconds, and the full batch is typically done in two to three minutes. Stop when the popping slows to one pop every two to three seconds. The exact time depends on the wattage, the batch size, and the kernel moisture.
Why are my kernels flying out of the chute?
Overfilling, a missing or loose lid, a tilted machine, or kernels that are too dry can all cause ejection. Reduce the batch to one-quarter cup and make sure the lid is seated correctly. Do not cover the chute with a cloth or plate. If the problem continues with a correct batch and a proper lid, check the kernel freshness.
How do I clean the machine without damaging it?
Unplug it, let it cool, and remove the lid and butter tray. Wipe the base with a damp cloth and dry it immediately. Do not immerse the base in water. Use a soft brush or dry cloth for the popping chamber. Wash the butter tray in warm soapy water and dry it fully before storage.
What causes chewy popcorn?
Chewy popcorn usually comes from trapped steam or old kernels. Do not cover the bowl tightly while the popcorn is still hot. Use a batch size that fits the chamber, and store kernels in an airtight container. If the popcorn is chewy within minutes of popping, try a fresher bag of kernels.
Can I use old kernels in a hot air popper?
You can try, but expect a lower pop rate. Old kernels have lost moisture, so they pop smaller and leave more unpopped kernels. Test a quarter-cup batch first. If more than 15 percent remain unpopped, use the kernels for a different purpose or replace them.
Do I need to preheat a compact hot air popcorn maker?
Usually no. The heating element and fan work from the moment you switch the unit on. If the manual recommends a short warm-up, keep it to 30 to 60 seconds. Do not run the machine empty for several minutes; that can overheat the chamber and shorten the life of the thermal cutout.
What is the difference between a hot air popper and a retro popcorn maker?
A hot air popper uses moving hot air and no oil in the chamber. A retro popcorn maker usually uses a kettle with oil and a stirring mechanism. The hot air model is faster to clean and easier for plain popcorn. The retro model is better for buttered theater-style popcorn and for a presentation counter where the machine is part of the display.
A compact hot air popper is not fragile; it is predictable when you keep the batch measured and the chamber dry.
Putting the Batch Together
Use this sequence the next time you fill the machine: place the popper on a level surface with clear vents, measure one-third cup of fresh kernels, turn the machine on, add the kernels, fit the lid, and listen for the first pop. When the popping slows to two or three seconds between pops, switch the unit off and pour the popcorn into a wide bowl. Let the machine cool, wipe the chamber, wash the butter tray, and store everything dry. That routine takes less time than reading the manual and gives you a batch that is crisp, evenly popped, and easy to repeat.
For commercial buyers, the same routine becomes a training standard. Write the batch size in grams on the station card. Keep a small scale nearby. Mark the cooling time between batches. Use a kernel supplier that can document moisture and turnover. A compact hot air popcorn maker is a simple product, but a simple product with a clear process is easier to support, easier to sell, and easier to keep in service. If you are planning a private-label program or a retail promotion, start with the batch size and the duty cycle, then build the packaging and the manual around them.
Consistent popcorn starts with a measured batch and ends with a clean, dry chamber.
Related products
Get in Touch
Your email address will not be published.
Required fields are marked *
Required fields are marked *
contact us
Have a project in mind?
Contact with us
Contact with us
We are happy to answer your questions. Please fill out this form
and one of our professional team will get back to you as soon as possible.
and one of our professional team will get back to you as soon as possible.
-
Company AddressNO.212 Qiaotou Road, Qiaotou Town, Cixi City Zhejiang Province
-
Tel:+86-574-63032602/63032605/63032682/63032681
-
E-mail:homease@homease.com.cn
huajun_sam@homease.com.cn
jayden@homease.com.cn
sunny@homease.com.cn
Copyright © Cixi Homease Electrical Products Co., Ltd. All Rights Reserved. China Small Home Appliances Manufacturer Food Equipment Factory
